Design Engineering for Equipment Foundations
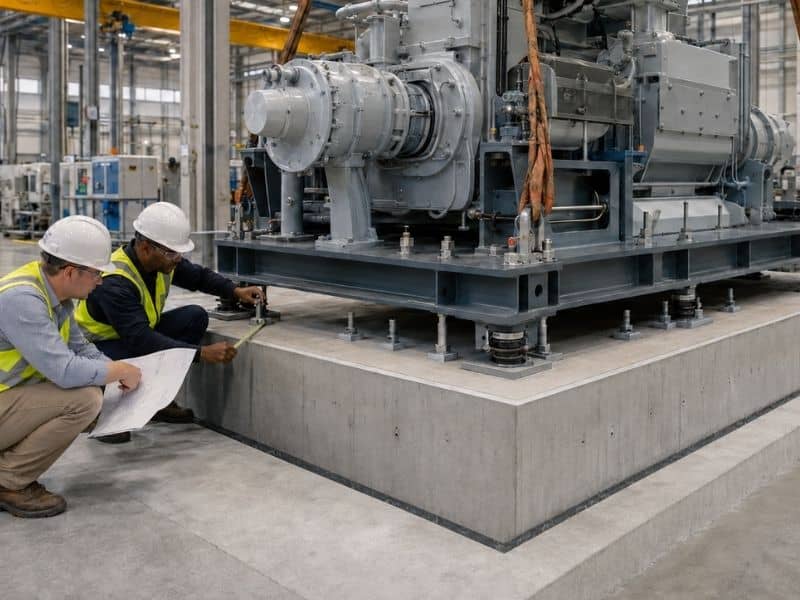
Heavy machines need more than a slab of concrete under them. A stamping press, a compressor, or a precision grinder does not just sit still. It moves. It shakes. It pushes and pulls on the ground beneath it. A foundation has to handle all of that, not just the machine’s dead weight. That is the job of design engineering. It matches a foundation to the real forces a machine makes while it runs.
This work happens often in Huntsville. New manufacturing plants keep opening in the area. Each one brings machines with their own weight, motion, and shake pattern. A foundation built for one machine rarely works for another without changes.
Design Engineering Starts With the Machine’s Operating Envelope
Weight alone does not tell an engineer much. Two machines can weigh the same. They can still need different foundations. That’s because weight does not show how a machine moves once it starts running.
To size a foundation right, an engineer asks the manufacturer for more details. This includes the machine’s shape and size. It includes the center of gravity. It includes how fast the machine runs during normal use. Startup and shutdown forces matter too. A motor spinning up, or a press slowing down, can push loads past normal levels. Imbalance loads matter as well. These come from parts that spin but are not perfectly balanced. Anchor locations matter. So does how much the machine can move before it loses alignment.
Plants that install special machines in Huntsville deal with this often. A press line or CNC machine may ship in from overseas. It often arrives with technical data. Engineers need to turn that data into a real concrete design. Skipping this step causes problems later. So does guessing at the numbers. Both can lead to cracking. Both can lead to misalignment. Both can wear down the machine faster than it should.
Separating Operating Frequency From Foundation Response
Rotating and reciprocating machines make repeated forces. This happens over and over, thousands of times an hour. Compressors do this. Stamping presses do this too. Each cycle sends a small jolt through the foundation. Those jolts add up over time.
Every foundation has a natural frequency. This means it shakes more at some speeds than at others, on its own. Design engineering looks at how close a machine’s running speed is to that natural frequency. If the two get too close, trouble starts. The foundation can start to make the shaking worse instead of calming it down.
Pouring more concrete does not fix this by itself. A bigger, heavier foundation changes the natural frequency. But it may not change it the right way. A smaller foundation, built with the right numbers, can work better than a huge one poured without any math. Mass matters. Stiffness matters. Shape matters. None of these should be guessed if the goal is a quiet, stable machine over its full life.
Turning a Vendor Anchor Pattern Into a Buildable Concrete Detail
Equipment makers give engineers an anchor pattern. This shows where the bolts need to go. On paper, it looks simple. Building it into real concrete takes more work than the drawing shows.
Anchor rods need space. Sleeves need space. Reinforcing steel needs space too. None of these parts can clash with each other. Baseplates need room around their edges. Steel bars need to stay far enough from anchor rods. If they sit too close, the concrete near the bolt gets weak. Edge distance matters too. A rod placed too close to the edge can crack the concrete under load.
This planning needs attention before the concrete truck shows up. Imported machines often leave little room to adjust later. Custom-built machines do the same. If the anchor pattern does not match the poured foundation, problems follow. Crews may need to drill new holes. They may need to chip out concrete. The job may get delayed. None of that is cheap. Checking anchor spots against the real foundation drawings, before the pour, prevents this trouble.
Treating Grout and Baseplate Contact as Part of the Load Path
Grout sits under a machine’s baseplate. It does not get much attention. But it plays a real part in how loads move through a foundation. It fills the gap between the machine’s base and the concrete below. That gap is rarely flat. It is rarely even across its full size.
Without good grout, a baseplate can rock a little under load. This happens even when the bolts are tight. That rocking wears down anchor bolts over time. It can throw off alignment on precision machines. Grout made for the job, placed the right way, gives the baseplate full contact with the concrete. Even contact matters. It lets the foundation take on the loads the machine sends down. Without it, stress builds up at just a few spots.
Getting this right takes two things. The grout type must match the load and the gap size. The install must match the maker’s clearance rules. This is a design question. It is also an install question. It is not just a normal concrete pour. Getting it wrong can weaken a foundation that was sized correctly in every other way.
Drawing an Isolation Boundary Around Precision Production Areas
Some equipment foundations need a clean break. They need space from the floor around them. They need space from nearby foundations too. Shaking does not stay in one spot. It travels through connected concrete. It can travel a good distance. It can reach places where that movement causes real trouble.
Measuring stations feel this. Calibration equipment feels this. Precision machining setups feel this too. A press running fifty feet away might seem harmless. Then a nearby measuring machine starts giving readings that do not match up. At that point, the shared foundation slab is often the cause.
Isolation joints can break that path. Gaps can too. So can separate foundation pours. But the right isolation detail depends on the machines involved. It depends on what the sensitive equipment actually needs to work well. A standard isolation gap, used without checking these details, can fail in both directions. It might be too small to matter. It might be bigger than needed. The real answer comes from looking at which machines sit near which processes. It comes from knowing how much shaking each one can handle. It does not come from an old detail pulled off a past project.
